BLOG
Top 10 Types of Metal Detectors in Pharmaceutical Industry
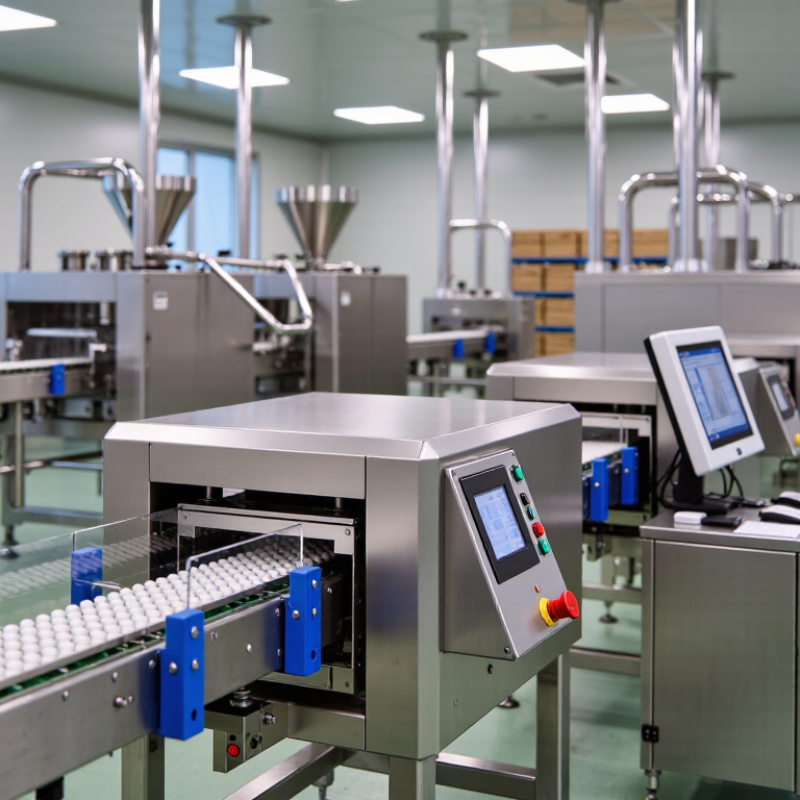
Metal contamination can damage pharmaceutical quality, equipment, and patient confidence. A metal detector in pharmaceutical industry operations therefore supports contamination control, process verification, and release confidence. It does not replace good manufacturing practice. It strengthens it.
Market research from Grand View Research identifies pharmaceutical manufacturing as a steadily modernizing sector, driven by automation, traceability, and stricter quality expectations. The FDA’s 2023 Quality Management Maturity program also emphasizes robust processes, reliable data, and continuous improvement. These priorities explain why manufacturers are evaluating more than one detection design. Tablets, capsules, powders, liquids, and packaged products create different inspection challenges.
Some systems inspect free-falling powders. Others monitor tablet presses, pipelines, conveyors, or finished packs. Their performance depends on aperture size, product effect, line speed, calibration, and reject confirmation. Small details matter. A poorly positioned sensor can miss a defect. Excessive sensitivity can create unnecessary rejects and production pressure.
This guide examines ten common metal detector types used across pharmaceutical manufacturing. It considers operating principles, suitable applications, hygienic design, validation needs, and practical limitations. The discussion follows expectations associated with FDA 21 CFR Parts 210 and 211, EU GMP principles, and USP General Chapter <1058> on analytical instrument qualification. These references do not make every detector suitable. Context remains essential.
No detector is perfect. That assumption deserves scrutiny. Real performance may change with moisture, temperature, packaging, or product conductivity. Operators must verify results under actual production conditions. The strongest choice is not always the most sensitive model. It is the system that delivers dependable detection, documented control, and consistent performance without compromising the process.
Core Principles of Metal Detection in Pharmaceutical Manufacturing
Top 10 Types of Metal Detectors in Pharmaceutical Industry
Core Principles of Metal Detection in Pharmaceutical Manufacturing
Metal detection protects pharmaceutical products from unintended metal fragments during processing and packaging. The system generates an electromagnetic field through a detection aperture. When metal enters this field, it changes the signal pattern. The detector then triggers an alarm or activates an automatic reject mechanism. Ferrous metals usually create strong responses, while stainless steel can be more difficult to detect.
Reliable performance depends on product characteristics, not only detector sensitivity. Dry tablets often provide stable signals. Powders, liquids, and products with high salt or moisture content may create product effects. These effects can resemble metal contamination. Operators must adjust frequency, aperture size, conveyor speed, and sensitivity carefully. Small test pieces should challenge the system at practical production points. The results need clear records and trained review.
In daily pharmaceutical operations, verification should occur before production, during the run, and after interruptions. A failed test requires controlled investigation, not a quick reset. No setting is perfect. Even experienced teams can overlook vibration, poor alignment, or a weak reject response. I have found that simple checks often reveal bigger process weaknesses. Clean equipment, stable product flow, and regular calibration support dependable detection. Human judgment still matters, especially when unusual products or packaging materials change the signal.
| No. | Detector Type | Core Operating Principle | Typical Pharmaceutical Application | Metal Contaminants Commonly Detected | Indicative Test-Sphere Sensitivity* | Key Advantages | Main Limitations | Important Validation and Process Controls |
|---|---|---|---|---|---|---|---|---|
| 1 | Conveyor Tunnel Metal Detector | A balanced electromagnetic field is generated across an aperture. A conductive or magnetic metal particle disturbs the field, and the signal is processed against a product baseline. | Bottles, cartons, sachets, tubs, and wrapped finished products moving on a conveyor. | Ferrous, non-ferrous, and stainless-steel particles. | Typically about 1.0–2.0 mm ferrous, 1.5–2.5 mm non-ferrous, and 2.0–3.0 mm stainless steel, depending on aperture and product effect. | Suitable for high-throughput inspection; can be integrated with automatic reject systems and production-line monitoring. | Sensitivity decreases as aperture size increases. Product moisture, salt, temperature, and orientation can affect performance. | Verify test pieces at the beginning, end, and defined intervals of each batch; confirm reject timing, reject-bin security, and conveyor speed. |
| 2 | Gravity-Fall Metal Detector | Free-falling powder, granules, or pellets pass through a detection coil. A metal particle changes the electromagnetic signal and activates a diversion valve or flap. | Powders, granules, excipients, active pharmaceutical ingredients, and nutraceutical ingredients transferred through vertical chutes. | Ferrous, non-ferrous, and stainless-steel fragments. | Commonly around 0.8–1.5 mm ferrous and 1.5–2.5 mm stainless steel under controlled free-fall conditions. | Compact design; low product-contact complexity; well suited to continuous bulk handling. | Requires stable product flow and correct installation height. Irregular flow, vibration, or bridging can reduce reliable detection. | Validate the reject mechanism under normal and maximum flow rates; inspect seals, chutes, and product-contact surfaces for residue accumulation. |
| 3 | Tablet and Capsule Metal Detector | A small-aperture balanced-coil system detects metal inclusions as individual tablets or capsules pass through a controlled product stream. | Tablet presses, capsule filling lines, tablet dedusters, and post-compression inspection. | Ferrous wear particles, stainless-steel fragments, and non-ferrous tooling debris. | Often approximately 0.3–0.8 mm ferrous and 0.5–1.2 mm stainless steel, subject to tablet size, speed, and formulation. | Designed for small-dose solid products; can inspect large quantities without opening primary packaging. | Small products may be difficult to separate reliably. Tablet orientation, vibration, dust, and mechanical tooling can influence results. | Use representative tablets or capsules with certified test pieces; verify detection after dedusting and monitor tooling wear and rejects. |
| 4 | Throat Metal Detector | Bulk product passes directly from a hopper, blender, or process vessel through a compact detection aperture before entering the next processing stage. | Tablet presses, vertical processing equipment, granulators, and powder transfer points. | Ferrous, non-ferrous, and stainless-steel contamination introduced by upstream equipment. | Typically about 0.8–1.8 mm ferrous and 1.5–2.5 mm stainless steel, depending on throat diameter and flow conditions. | Protects downstream equipment and product; uses limited floor space and can be installed close to the source of contamination. | Small apertures may restrict throughput. The detector must be carefully isolated from vibration and electromagnetic interference. | Confirm grounding, vibration isolation, line clearance, sanitary connections, and fail-safe operation during loss of power or compressed air. |
| 5 | Pipeline Liquid Metal Detector | A liquid or semi-liquid product flows through a non-metallic or suitably designed pipe section surrounded by detection coils. Metal signals trigger a hygienic diversion valve. | Syrups, suspensions, creams, gels, liquid medicines, and other pumpable pharmaceutical products. | Ferrous, non-ferrous, and stainless-steel particles. | Frequently around 1.0–2.5 mm ferrous and 1.5–3.5 mm stainless steel, depending on conductivity, viscosity, and pipe diameter. | Supports closed processing; reduces operator exposure and can be connected to clean-in-place systems. | Product conductivity and temperature can create strong product effects. Pulsation, air bubbles, and unstable flow may cause false signals. | Validate at actual flow, temperature, and viscosity; verify valve diversion volume, hygienic design, cleaning performance, and pressure limits. |
| 6 | Pipeline Powder Metal Detector | Powder moving through a pneumatic or gravity pipeline passes through an electromagnetic detection zone, with contaminated material diverted without opening the process line. | Pneumatic transfer of active ingredients, excipients, dry blends, and powdered formulations. | Ferrous, non-ferrous, and stainless-steel particles from mills, screens, valves, and conveying equipment. | Commonly approximately 1.0–2.0 mm ferrous and 1.5–3.0 mm stainless steel, depending on pipe diameter and powder characteristics. | Enables in-line inspection in contained systems; protects downstream filling and compression equipment. | Pneumatic velocity, powder density, static electricity, and pipeline buildup may affect signal stability and reject accuracy. | Assess air velocity, grounding, pressure, product residence time, filter condition, and the ability of the reject device to handle the full contaminated portion. |
| 7 | Vertical Form-Fill-Seal Metal Detector | A detector is positioned around the product path of a vertical packaging machine. The electromagnetic field examines the falling product before or during bag formation. | Sachets and pouches containing powders, granules, tablets, or capsules. | Ferrous, non-ferrous, and stainless-steel contamination in bulk product or packaging streams. | Usually about 1.0–2.0 mm ferrous and 1.5–3.0 mm stainless steel, influenced by product effect and film configuration. | Inspects product before final sealing; can reduce the risk of sealing contaminated material into finished packs. | Packaging-film components, sealing jaws, vibration, and intermittent product flow may complicate calibration. | Test with the actual film and product; verify synchronization between detection, sealing, coding, and reject functions. |
| 8 | Ferrous-in-Foil Detector | A specialized magnetic or electromagnetic system is optimized to detect ferrous contamination inside aluminum foil or metallized packaging, where conventional balanced-coil systems may be unsuitable. | Aluminum-blister packs, foil sachets, foil pouches, and other metalized pharmaceutical packages. | Primarily ferrous steel particles; detection of non-ferrous and stainless steel is generally limited. | Often approximately 0.8–2.0 mm ferrous, depending on foil thickness, pack geometry, and detector configuration. | Allows inspection of products after packaging in foil-based materials; useful where standard electromagnetic detection is masked by the package. | Usually cannot provide the same multi-metal capability as a standard balanced-coil detector. Aluminum thickness and package orientation are critical. | Validate with test pieces inside representative foil packs; check pack orientation, foil specification, magnetic interference, and rejection traceability. |
| 9 | Hygienic Washdown Conveyor Detector | A sealed balanced-coil detector operates within a sanitary conveyor designed to withstand frequent cleaning, moisture, and chemical exposure. | Moisture-sensitive or liquid-containing products, coated tablets, wet granules, and products processed in controlled washdown areas. | Ferrous, non-ferrous, and stainless-steel particles. | Commonly about 1.2–2.5 mm ferrous and 2.0–3.5 mm stainless steel, depending on aperture, belt width, and product characteristics. | Supports hygienic production; sealed construction helps protect electronics during routine sanitation. | Water films, cleaning chemicals, belt moisture, and temperature changes can temporarily increase product-effect signals. | Confirm ingress protection, drainage, cleanability, drying requirements, belt tracking, sanitation chemicals, and post-cleaning performance. |
| 10 | Multi-Frequency Metal Detector | The system uses two or more operating frequencies or advanced signal-processing methods to improve discrimination between product effects and metal signals. | Products with high moisture, salt, conductivity, or variable formulations, including coated and ready-to-pack medicines. | Ferrous, non-ferrous, and stainless-steel contamination, with improved performance on difficult products. | Typical performance may range from about 1.0–2.0 mm ferrous and 1.5–3.0 mm stainless steel, but must be established by product-specific validation. | Better control of product effect; can improve sensitivity across products with different electrical characteristics. | Requires careful setup, product calibration, and changeover management. It does not eliminate the need for physical test verification. | Create product-specific settings; validate worst-case formulation, temperature, moisture, packaging, line speed, and changeover procedures. |
Ten Main Metal Detector Types for Pharmaceutical Products
Pharmaceutical metal detection requires more than a sensitive sensor. Product form, packaging, speed, and cleaning routines all influence performance. Ten main metal detector types are commonly considered: conveyor, gravity-fall, pipeline, tablet, capsule, bottle, vertical-chute, bulk-hopper, checkweigher-integrated, and rotary-indexing detectors. Each configuration suits a different production point.
Conveyor detectors inspect sealed cartons, bags, or trays as products pass through an aperture. Gravity-fall and bulk-hopper models examine powders and granules moving downward. Pipeline systems monitor liquids, creams, or suspensions inside closed lines. Tablet and capsule detectors use compact channels for high-speed dosage inspection. Bottle detectors handle containers after filling or capping. Vertical-chute systems suit free-falling products with limited floor space. Checkweigher-integrated units combine weight control with metal detection. Rotary-indexing detectors inspect products in controlled positions, often during filling or packaging.
Selection should follow a documented hazard analysis, not habit. Stainless steel, ferrous metal, and non-ferrous metal may respond differently. Product temperature, moisture, salt content, and foil packaging can reduce sensitivity. Testing should use certified test pieces at realistic speeds and product loads. Reject devices also need challenge testing, secure collection, and traceable records. Cleaning access matters, especially around seals and narrow product channels. No detector is perfect. False rejects still deserve investigation. A practical system may protect quality well, yet require better product trials before routine validation.
Detector Types for Tablets, Capsules, Powders, and Granules
Top 10 Types of Metal Detectors in Pharmaceutical Industry
Metal detection changes with the product’s shape, density, and movement. Tablets commonly use press-throat detectors, tablet-deduster detectors, chute detectors, conveyor detectors, and rotary discharge detectors. These systems inspect tablets after compression, coating, or dedusting. Their narrow product paths help maintain sensitivity. They also reduce product buildup around the inspection point.
Capsules may pass through capsule-polisher detectors, vertical chute detectors, vibratory-feed detectors, conveyor detectors, or combined dedusting systems.
Powders and granules require different handling. Gravity-fall detectors inspect free-flowing material from hoppers. Vertical pipeline detectors suit controlled powder transfer. Pneumatic-line detectors monitor product moving through enclosed air systems. Bulk-feed detectors protect larger batches before filling or blending. These are ten practical configurations across common pharmaceutical processes.
Installation experience matters. A detector should match the feed rate, product temperature, moisture, and packaging stage. Stainless steel contact parts support hygienic cleaning. Automatic rejection must prevent accepted product from mixing with rejected material. Validation should include ferrous, non-ferrous, and stainless-steel test pieces at realistic operating speeds. Small details matter.
No setup is perfect. Product effect can reduce sensitivity, especially with conductive or damp powders. A clean test result may still hide poor placement or unstable flow. Operators should record test results, investigate repeated alarms, and review performance after maintenance. Human judgment remains important, even with automated inspection.
Detector Types for Liquids, Pipelines, Foils, and Packaging Lines
Metal detectors in pharmaceutical production are selected by product behavior, not by appearance alone. Ten common configurations include liquid-line, pipeline, gravity-feed, free-fall, conveyor, tablet, capsule, foil-seal, cap, and finished-pack detectors. Each design creates a different inspection challenge. A liquid detector must handle conductive products, such as syrups or saline solutions, without producing excessive false alarms. Pipeline systems need stable pressure and smooth product flow. Small changes matter.
Foil packaging needs special attention. Aluminum foil can block conventional detection, so a foil-compatible system often inspects the product before sealing. Foil-seal detectors can also check the finished pack when the package structure permits reliable signal processing. Conveyor detectors inspect cartons, blister packs, bottles, and sachets. Packaging-line units should reject contaminated products quickly and record the event clearly. In practice, poor alignment causes more trouble than many teams expect. It deserves regular review.
Tips: Test with certified ferrous, non-ferrous, and stainless-steel standards. Place test pieces at the product’s most difficult position. Check sensitivity during startup, cleaning, speed changes, and product changeover. For liquid and pipeline applications, confirm that pumps do not create unstable flow. Keep inspection records with lot details and rejection reasons. Clean apertures and sensors according to the validated procedure. Do not rely on factory settings alone. Real production conditions can behave differently. A detector may pass yesterday’s test and fail today’s test if temperature, moisture, foil position, or product density changes. That is why trained operators, documented verification, and periodic calibration remain essential.
Selection, Validation, Hygiene, and Compliance Requirements
Top 10 Types of Metal Detectors in Pharmaceutical Industry
Metal detector selection depends on product form, line speed, packaging, and contamination risk. Common options include gravity-feed, conveyor, pipeline, tablet, capsule, vertical-drop, foil-sensitive, bulk-product, liquid-product, and combination systems. Selection should begin with a documented hazard assessment, not a catalog comparison. Powders may require different aperture control than dense tablets or viscous liquids.
Small details matter. Consider product effect, temperature, pressure, cleaning access, and reject mechanism. In practice, a detector that performs well during factory trials may struggle after cleaning or product changeover.
Validation should demonstrate reliable detection at the intended operating speed. Use traceable ferrous, non-ferrous, and stainless-steel test pieces at defined positions. Record sensitivity, belt speed, product temperature, reject timing, alarm response, and failed-test actions. Repeat challenges after start-up, stoppage, sanitation, and major maintenance.
Do not treat one successful test as proof. That assumption is easy to make, and often weak. Approved protocols, training records, calibration evidence, and deviation investigations support defensible decisions. Requirements differ by market, so compliance teams should confirm applicable pharmaceutical quality standards.
Hygienic design should minimize ledges, exposed threads, hollow sections, and water traps. Use smooth, cleanable contact surfaces and accessible inspection points. Inspect seals, belts, guides, and reject bins during every sanitation cycle.
Drying is not optional. Moisture can encourage residue buildup and weaken inspection reliability.
Operators should verify cleaning effectiveness with documented checks, not visual confidence alone. Periodic reviews should examine false rejects, recurring alarms, product changes, and maintenance findings.
A practical gap may remain: teams sometimes validate detection thoroughly but overlook the hygiene of surrounding equipment.
Related Posts
-
Top Metal Detectors for the Pharmaceutical Industry?
-
Top Metal Detectors for the Pharmaceutical Industry?
-
What Is a Metal Detector for the Pharmaceutical Industry?
-
Why X Ray Inspection Matters in the Food Industry?
-
Top 10 X Ray Food Inspection Systems for Global Buyers?
-
Why Food X-Ray Technology is Revolutionizing Food Safety and Inspection?