How to Choose Food X Ray Inspection Equipment in 2026?
Choosing food x ray inspection equipment in 2026 requires more than comparing prices or detector sizes. Modern food lines face changing products, faster speeds, smaller packaging, and stricter customer expectations. The right system must identify dense physical contaminants while protecting product quality and production efficiency. It should also provide clear images, stable calibration, reliable rejection, and usable inspection records.
W. Edwards Deming, a respected quality expert, wrote, “Quality comes not from inspection, but from the improvement of the production process.” This principle remains valuable when selecting food x ray inspection equipment. An X-ray unit should support prevention, not merely detect failures at the end of a line. Buyers should examine sensitivity tests, product-effect performance, belt speed, reject confirmation, sanitation design, software access, and service response. Small details matter. A poorly positioned reject bin can undermine an expensive inspection system.
Experience also matters. Ask suppliers to test your actual products, including dense sauces, wrapped multipacks, glass jars, and uneven packages. Request documented results under realistic operating conditions. Do not rely only on a showroom demonstration. No machine is perfect. That assumption deserves challenge.
A strong decision balances detection capability, total ownership cost, operator training, maintenance access, and future expansion. It should fit your facility, not just your brochure. Independent validation can strengthen confidence, especially when product density changes across seasonal batches. This guide explains the practical questions, technical specifications, and evaluation steps that help food manufacturers choose dependable food x ray inspection equipment for 2026.
Define Food Safety Risks and X-Ray Inspection Objectives
How to Choose Food X-Ray Inspection Equipment in 2026?
Define Food Safety Risks and X-Ray Inspection Objectives
Food safety objectives should start with real hazards, not equipment features. The World Health Organization estimates that contaminated food causes 600 million illnesses and 420,000 deaths globally each year. Physical contamination remains a practical concern in processed foods. Common risks include glass, metal, stones, dense bone, and damaged packaging components. X-ray systems can detect many dense foreign materials, but they do not reliably identify pathogens or every low-density contaminant. That limitation must remain visible during planning.
Build the inspection objective around your product and line conditions. Record product density, package dimensions, temperature, moisture, speed, and expected defects. Define measurable targets, such as detection sensitivity, false-rejection rate, inspection coverage, and automatic reject response time. Test products at the fastest operating speed. Include the smallest realistic contaminant in the worst product position. Codex Alimentarius recommends science-based hazard analysis, while HACCP principles support linking each control to a defined risk.
Practical experience shows that clean test images can mislead. A product may pass during commissioning but fail after recipe, film, or speed changes. Some dense ingredients also create confusing images. No target is perfect. Review rejected packs, challenge the system regularly, and document every adjustment. The objective is not simply finding contamination. It is creating dependable evidence that each critical control performs under real production pressure.
Compare X-Ray Detection Technologies and Equipment Capabilities
When choosing food X-ray inspection equipment in 2026, compare detection technology before comparing price. Single-energy systems suit uniform products with clear density differences. Dual-energy systems separate overlapping materials more effectively, especially in dense or layered foods. They can improve sensitivity, but they may require stronger process control and operator training. Better technology is not automatically better for every line.
Detector resolution affects the smallest detectable contaminant and image clarity. A narrow beam can support detailed inspection, while a wider aperture handles larger packages. Check conveyor speed, product spacing, and reject timing together. A fast machine with poor timing still creates risk. I have seen accurate detection weakened by unstable product flow. That detail is easy to miss.
Equipment capability also includes hygiene and verification. Choose corrosion-resistant construction, smooth surfaces, and cleaning access around the conveyor and reject area. Software should record images, alarms, test results, and user actions for traceability. Automatic calibration can reduce routine effort, but operators still need scheduled checks with suitable test pieces. No system is perfect. False rejects deserve attention, too. Excessive sensitivity may waste good food and hide process weaknesses. Before purchase, test real products at normal temperature, speed, packaging, and moisture levels. A controlled factory trial often reveals limitations that brochures cannot show.
Evaluate Product, Packaging, and Production Line Compatibility
When choosing food X-ray inspection equipment in 2026, start with the product, not the machine brochure. Frozen meals, liquid sauces, and dense cheese create different inspection conditions. Product temperature, moisture, thickness, and density can affect image contrast. Test representative samples, including normal variation and difficult packs. A clean result on one sample proves little. It is not enough.
Packaging must also match the inspection system. Foil, metalized film, glass, and thick cartons can change detection performance. Check package dimensions, seal areas, orientation, and spacing between products. Ask for tests using final packaging, not empty trays. Small air gaps may shift during transport. That detail is easy to miss. I have seen teams approve equipment before testing their fastest line speed. A later trial exposed unstable spacing and inconsistent rejects.
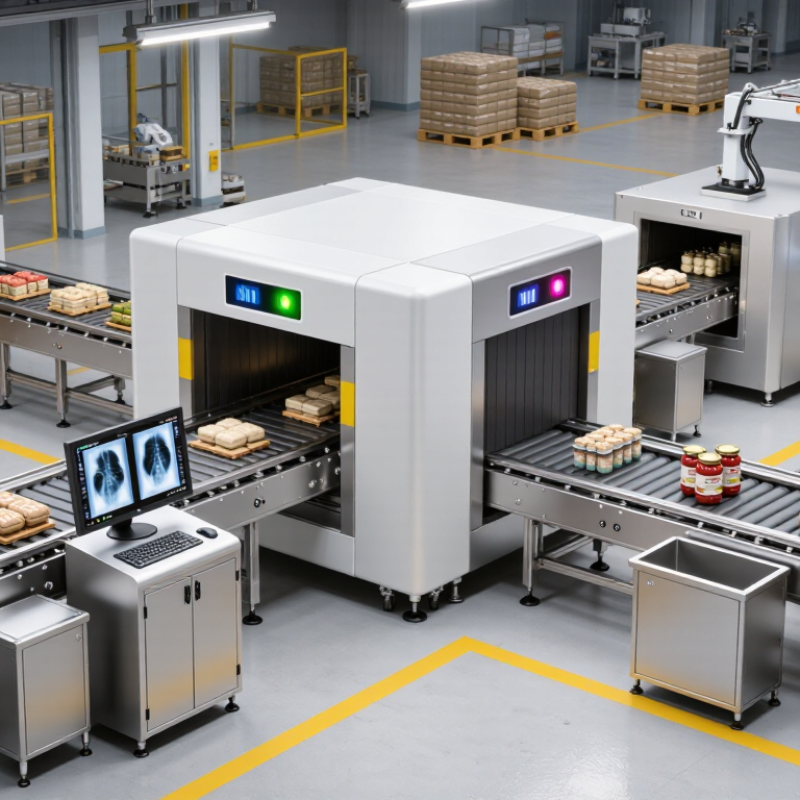
Production line compatibility is equally practical. Confirm conveyor height, belt width, throughput, washdown conditions, and available floor space. The reject device should remove suspect products without disturbing adjacent packs. Sensors, guarding, and emergency stops must fit the existing control system. Request documented sensitivity results, calibration procedures, training, and service response times. Keep records for each product and package format. Leave room for maintenance. This is often underestimated. Before purchase, run a site trial under real operating conditions.
Assess Detection Accuracy, Compliance, Maintenance, and Total Cost
How to Choose Food X-Ray Inspection Equipment in 2026?
Detection accuracy should match your real production conditions. Test products with dense ingredients, overlapping packs, foil layers, and uneven filling levels. A clean laboratory sample may produce flattering results. I would not trust brochure figures alone. Run trials using your own products, packaging, line speed, and reject settings. Measure missed contaminants, false rejects, image quality, and inspection stability across several shifts. Short test pieces matter. Keep the results for future audits and supplier comparisons.
Compliance requires more than a certificate in a sales folder. Check whether the equipment supports applicable food-safety rules, customer standards, traceable records, secure access, and documented verification. Operators should understand test routines and alarm responses without guessing. Maintenance also affects compliance. Look for hygienic surfaces, easy belt removal, clear cleaning access, remote diagnostics, and practical calibration procedures. Ask how quickly technicians respond and whether critical spare parts are locally available. A machine that stops for days is expensive, even when its purchase price looks attractive.
Calculate total cost over its working life. Include installation, line integration, training, energy use, software fees, planned servicing, rejected product, and production downtime. A cheaper unit may create higher costs through frequent false rejects or difficult cleaning. Request a written service schedule and realistic uptime assumptions. Review the figures with maintenance and quality teams, not only purchasing. Their concerns may expose a weakness that a polished demonstration hides. Test the reject mechanism at full speed, because performance can change when the factory becomes busy.
How to Choose Food X-Ray Inspection Equipment in 2026?
Assess detection accuracy, compliance, maintenance, and total cost using a transparent 100-point procurement model.
Detection accuracy receives the highest weighting because performance should be verified with representative products and test pieces. Compliance covers applicable food-safety, electrical, radiation-safety, HACCP, and customer-audit requirements. Maintenance and total cost include cleaning access, calibration, service response, spare parts, energy use, and the expected operating life. These are normalized planning weights, not manufacturer or market-share data.
Select, Install, Validate, and Optimize the Inspection System
How to Choose Food X-Ray Inspection Equipment in 2026?
Selection should begin with actual product conditions, not a glossy specification sheet. Record package size, density, temperature, line speed, and likely contaminants. A frozen meal and a glass jar need different test methods. Ask for sensitivity data using realistic samples. Tiny defects can disappear in dense products. That detail matters. Experienced teams also check software records, image review, reject timing, and cleaning access. A machine that detects well but slows sanitation will create operational pressure.
Installation needs a measured layout. Leave room for belt access, reject bins, guarding, and electrical service. Align the conveyor carefully; a slight transfer gap can cause product tipping. Validate performance during normal production, not only during a quiet trial. Use certified test pieces at agreed positions and speeds. Challenge the system after start-up, changeovers, and cleaning. Record every result, including failures and retests. Validation should involve quality, maintenance, and line operators. Each group sees a different risk. We once overlooked glare on an inspection screen. It did not affect detection, but it slowed decisions.
Optimization comes from trends, not guesswork. Review false rejects, missed alarms, downtime, and product temperature each week. Adjust settings only after confirming the cause. Excessive sensitivity may waste good product; weak settings may hide a developing fault. Train operators to respond consistently and document deviations immediately. Recheck performance after film changes, recipe changes, belt replacement, or software updates. Keep procedures practical.